
The Froth Phase Is Part of the Separation Process
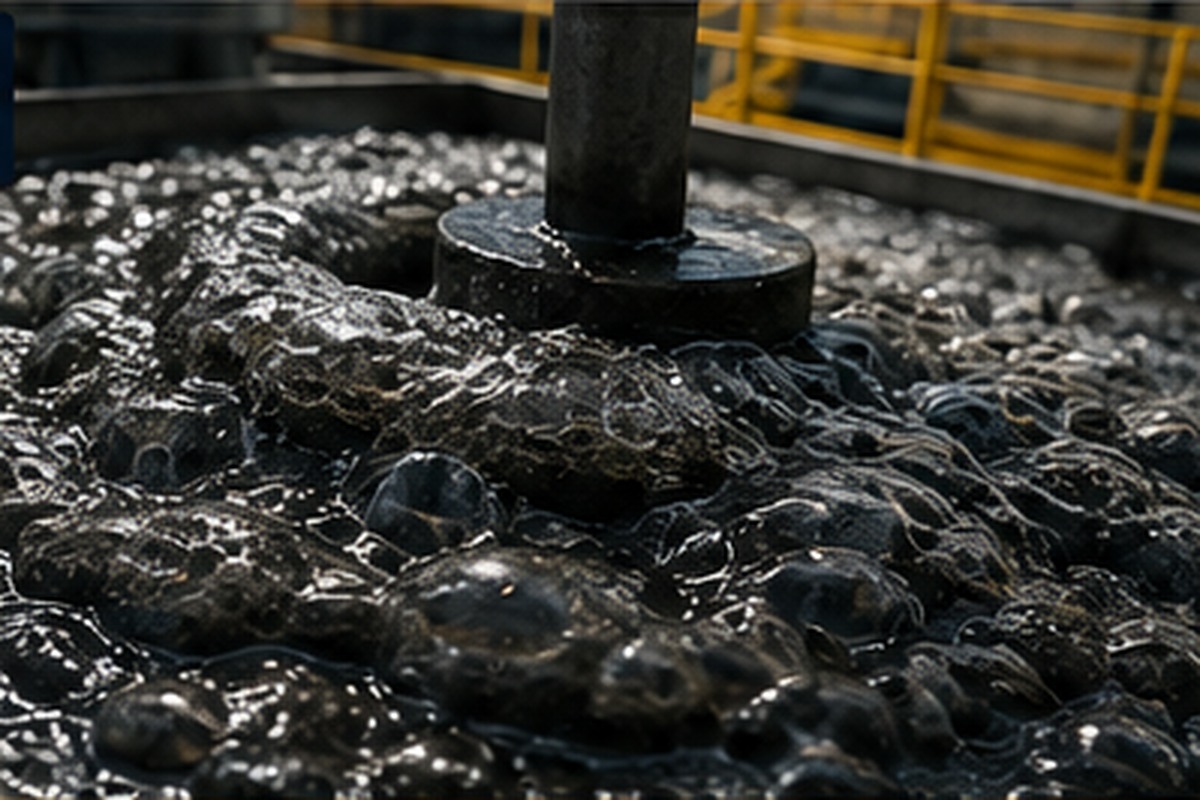
In froth flotation, valuable mineral particles first need to attach to bubbles, but they also need to survive transport through the froth and reach the concentrate launder.
Frothers help control bubble formation and froth characteristics. Their influence can be seen in bubble size, froth stability, mobility and the ability of the froth to carry mineral to the concentrate stream. A useful next step is our guide on flocculants in Mineral Processing: How Polyacrylamide Supports Solid-Liquid Separation, which looks at the related practical considerations in more detail.
Plant assessments routinely consider froth stability, bubble size, froth transport and reagent dosage when diagnosing flotation performance.
A Stable Froth Is Not Simply the Most Persistent Froth
The objective is not to create foam that lasts as long as possible. The froth needs characteristics appropriate to the mineral, circuit stage, cell design and required grade-recovery balance. A useful next step is our guide on how to Select Activated Carbon for Gold Recovery, which looks at the related practical considerations in more detail.
If froth is too unstable, valuable mineral may drop back before reaching the launder. If it is excessively persistent or poorly selective, the circuit may carry unwanted material or become difficult to operate.
That is why frother selection belongs to metallurgical test work and plant optimisation, not a generic purchasing decision.
Different Frothers Behave Differently
Commercial frothers vary in chemistry and frothing characteristics. Products that look equivalent on a quotation may produce different bubble populations and froth behaviour in the plant.
Ore characteristics also change. A frother that performs well on one feed may need different dosage or may not be optimal as mineralogy, particle size or water chemistry changes.
Procurement should therefore buy against an approved specification and avoid untested substitution based only on price or product description. A useful next step is our guide on xanthates in Mineral Processing: What Procurement Teams Should Know, which looks at the related practical considerations in more detail.
Dosage and Performance Determine Economic Value
Unit price is easy to compare, but reagent cost depends on how much product the circuit consumes and what performance it delivers.
A useful trial should monitor dosage together with recovery, concentrate grade, froth behaviour and operating stability. Process optimisation can also reduce unnecessary reagent consumption when the circuit is stabilised and controlled effectively. A useful next step is our guide on lime in Gold Processing: pH Control, Consumption and Supply Planning, which looks at the related practical considerations in more detail.
The commercial winner is the product that contributes to the required metallurgical outcome at an acceptable total cost, not necessarily the cheapest drum.
Test Work Creates a Safer Basis for Change
Bench-scale flotation testing allows reagent type, dosage and conditioning conditions to be varied in a controlled environment. Pilot work can provide a closer representation of continuous plant behaviour when the decision warrants it.
Laboratory batch flotation does not reproduce every aspect of an industrial continuous circuit, which is an important limitation when interpreting supplier trials.
For major changes, procurement should work with metallurgy to define what evidence is required before a new frother becomes an approved plant reagent.
Water Chemistry and Feed Changes Matter
Flotation performance is affected by multiple interacting variables, including feed grade, liberation, particle size and mineralogy. Process water conditions can add another layer of variability.
When a plant sees a change in froth behaviour, the frother itself may not be the only cause. Technical teams should review operating conditions before concluding that a batch is defective.
Good supplier traceability still matters because it allows reagent changes to be separated from process changes during troubleshooting.
Specify What Procurement Actually Needs
The RFQ should identify the approved frother or technical specification, required quantity, packaging, delivery schedule, delivery point and documentation.
If alternatives are permitted, the supplier should understand that technical approval or test work is required before substitution.
Procurement should also confirm lead time and stock availability. A technically excellent frother is of little use if the mine cannot obtain it consistently.
Treat Supply Continuity as Part of Flotation Performance
A shortage can force a plant to reduce throughput, accept an untested substitute or change operating strategy. Those consequences can outweigh modest savings achieved through aggressive inventory reduction.
Safety stock should reflect actual consumption, lead-time variability and the availability of approved alternatives.
By combining metallurgical approval with supplier performance tracking, mining companies can protect both flotation performance and commercial flexibility. A useful next step is our guide on how Mining Companies Can Reduce Chemical Supply Interruptions, which looks at the related practical considerations in more detail.
Discuss Your Mining Chemical Requirement With Aviv Kitov Group
Aviv Kitov Group supports mining and industrial organisations in Ghana with specialised chemical sourcing across regional and international markets. For the wider context, our guide on mining Chemicals in Ghana: A Practical Guide to Reagents, Supply and Process Risk brings the main procurement considerations together in one place.
For a useful supply assessment, provide the product, technical specification or approved grade, quantity, packaging, delivery location and required date.
Our team can then assess sourcing options against the commercial and operational requirement.
For the fastest assessment, include:
- product or reagent required
- technical specification or approved grade
- quantity
- preferred packaging
- delivery location
- required delivery date
Pingback: Xanthates Mining Chemicals: Procurement Guide
Pingback: Sodium Cyanide Ghana Mining: Procurement & Supply Guide